01Modern Industrial Steam Generation and Management Systems
Steam is one of the main driving forces of the modern industrial energy sector. Thanks to precise temperature control, safety and high energy-transfer efficiency, it is an indispensable resource in sectors such as pharmaceuticals, the chemical industry, food processing and heavy industry. However, efficient operation of steam systems requires complete synchronization of the generation, distribution and control processes.
02The Steam Life Cycle and Infrastructure
An industrial steam network is a complex engineering system consisting of several key stages:
- Steam generating plants (generation): the "heart" of the system, where modern, high-efficiency industrial boiler houses carry out the phase change of water. The process requires optimized fuel combustion and chemical water treatment to ensure long system service life.
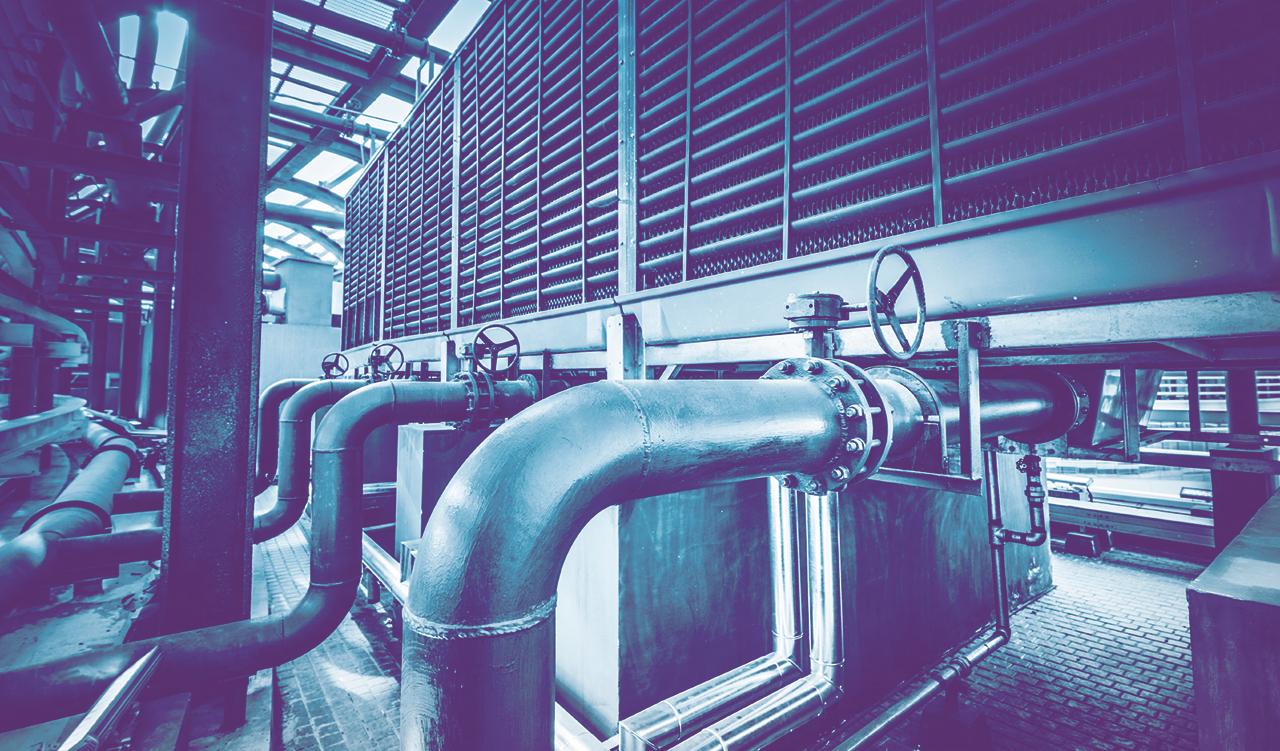
- Distribution networks: a system of high-pressure pipelines that delivers steam to the points of use. Flawless thermal insulation and properly functioning pressure reducing stations (PRV) are critical here, so that energy reaches the consumer at precise parameters and without losses.
- Condensate lines and steam traps: once the steam has given up its heat and condensed, special condensate traps discharge it from the system without letting expensive live steam escape.
03Modern Process Management and Control Systems
Today, the efficiency of industrial systems is unthinkable without high-tech automation. Modern industrial plants integrate SCADA and BMS (Building Management System) systems, PLCs (programmable logic controllers) and smart valves. Telemetry sensors monitor pressure, temperature and flow in real time. This allows operators to respond to changes instantly, prevent water hammer, reduce the risk of unplanned shutdowns (downtime) and manage processes with the highest precision.
04Energy Saving and Heat Recovery
The greatest potential in steam systems lies precisely in recovering energy and reusing it. Flash steam recovery, returning condensate to the boiler with condensate pumps, and economizers that use the energy of flue gases play a vital role in the overall efficiency of the system.
Why This Is Critically Important
- For the plant (local scale): returning hot condensate to the boiler significantly reduces the consumption of both cold make-up water and the fuel needed to heat it. Implementing energy-saving technologies translates directly into a dramatic reduction in operating expenses (OPEX), increases the plant's profitability and extends the service life of the infrastructure.
- On a global scale: industrial energy efficiency is no longer just a financial matter. Lower fuel consumption means a direct, large-scale reduction in carbon (CO2) emissions. By optimizing steam systems, heavy industry takes a significant step toward decarbonization and toward meeting global environmental challenges, thereby complying with international environmental standards.
Let's take a deeper look at the technical details of industrial steam systems:
05Part 1: Steam Generation, Distribution and Control Equipment (Types)
A steam system consists of many critical components. Each has a specific purpose and is selected according to the requirements of the production process (pressure, temperature, flow rate).
1. Steam Generation: Industrial Steam Boilers
Industry mainly uses two types of steam boiler; the choice between them depends on the required pressure and capacity:
- Fire-tube boilers: in this type of boiler, hot gases (from combustion) pass through tubes immersed in a water-filled vessel. They are distinguished by a large water volume, which allows them to cope well with sharp peak changes in steam demand. They are used in low- and medium-pressure systems (up to 25 bar).
- Water-tube boilers: here it is the other way around — water flows inside the tubes, while the flame and hot gases heat them from the outside. This design makes it possible to achieve very high pressures (100+ bar) and enormous capacities. They are commonly found in thermal power plants and heavy chemical industry.
2. Distribution Systems and Pressure Reduction
The boiler produces steam at high pressure (to reduce pipe diameters during steam transport); however, at the steam-using equipment (e.g. an evaporator or heat exchanger), steam is more efficient at low pressure, because at low pressure steam can release more latent heat.
- Pressure reducing valves (PRV): a device that reduces and stabilizes steam pressure before it is supplied to the consuming equipment. There are direct-acting valves (simple, for small flow rates) and pilot-operated valves (for high accuracy and large flow rates).
3. Condensate Traps / Steam Traps
One of the most important elements of the system. Their purpose is to discharge the condensate (water) and air formed in the system without passing "live" (useful) steam. They fall into 3 main categories:
- Mechanical (this type has two sub-types: float type and inverted bucket type): operate on the difference in density. Ideal for continuous discharge of large amounts of condensate.
- Thermodynamic: operate on changes in dynamic pressure. They are compact, withstand water hammer and are hard to freeze (used for draining outdoor steam mains).
- Thermostatic: operate on the temperature difference between steam and condensate.
06Part 2: Energy Efficiency, Condensate Return and Energy-Saving Technologies
In industrial steam systems, reducing energy losses is directly linked to a company's profitability and to the environment. The main focus of heat recovery is the management of hot condensate.
When steam gives up its heat, it turns into condensate — extremely pure, demineralized hot water (often 90°C – 100°C). Discharging it to the sewer wastes both thermal energy and expensive chemically treated water.
Technical Means for Condensate Recovery
- Condensate Recovery Units: conventional electric pumps handling hot water (90°C+) often suffer from cavitation (boiling inside the pump), which damages them. That is why specially designed electric pumps or mechanical (steam-driven) pumps are used. A mechanical pump uses the pressure of the steam itself (or compressed air) to return condensate to the boiler house and requires no electricity.
- Flash Steam Recovery: when high-pressure condensate passes to a lower pressure, part of the water instantly boils and turns into so-called "flash steam". Special separator vessels (flash vessels) collect this steam and supply it to low-pressure consumers (e.g. space heating, water preheating).
- Economizers: the temperature of the gases leaving the boiler stack often reaches 200°C–300°C. An economizer is a heat exchanger that uses this otherwise lost energy to preheat make-up or returned water before it enters the boiler. Every 6°C increase in boiler feedwater temperature reduces fuel consumption by approximately 1%.
07Part 3: Economic Benefit (A Worked Example)
Consider a medium-sized plant operating a steam boiler with a capacity of 10 tonnes/h (10,000 kg/h). The system operates 6,000 hours per year.
Scenario A (inefficient): condensate is not returned. The boiler is fed with cold, fresh water at 15°C, which requires mechanical filtration, chemical treatment and heating.
Scenario B (energy-efficient): 80% of the condensate produced (8,000 kg/h) is returned to the boiler. The temperature of the returned water is 90°C.
| Parameter | Scenario A (no condensate return) | Scenario B (80% return) | Difference (savings) |
|---|---|---|---|
| Make-up (cold) water at 15°C | 10,000 kg/h | 2,000 kg/h | 8,000 litres of water saved per hour |
| Energy required to heat the water (from 15°C to 90°C) | Spent on the full volume | Saved on 80% of the volume | ~700 kW of thermal energy (every hour) |
| Annual water savings (6,000 h) | 0 m³ | 48,000 m³ | 48,000 tonnes of clean water saved |
| Annual energy savings | 0 kWh | ~4,200,000 kWh | Huge savings on natural gas (see the calculator below) |
(In addition, the cost of chemical water treatment (reagents) falls by at least 80%, as does the need for bottom and surface blowdown of the boiler, which further increases efficiency.)
Dear visitors (engineers, plant managers), to give you a better sense of the scale of the financial benefit involved, please see the interactive calculator below. You can change the inputs to match the parameters of your hypothetical or real plant and see the amount of energy and money saved in real time:
Interactive calculator
Savings from returning condensate to the boiler
Parameters
Annual savings
Annual financial savings
557 867₾
Money saved on fuel
Heat energy saved per year
4 648 889kWh
Clean water saved per year
48 000m³
Chemical treatment costs fall too